Production

The manufacture of parts, components and products via different composite solutions is an area that is rapidly growing today. Despite this, the level of knowledge is relatively low in general, perhaps due to industrial and design engineering traditions, but also because composite is another way of thinking and solving problems.

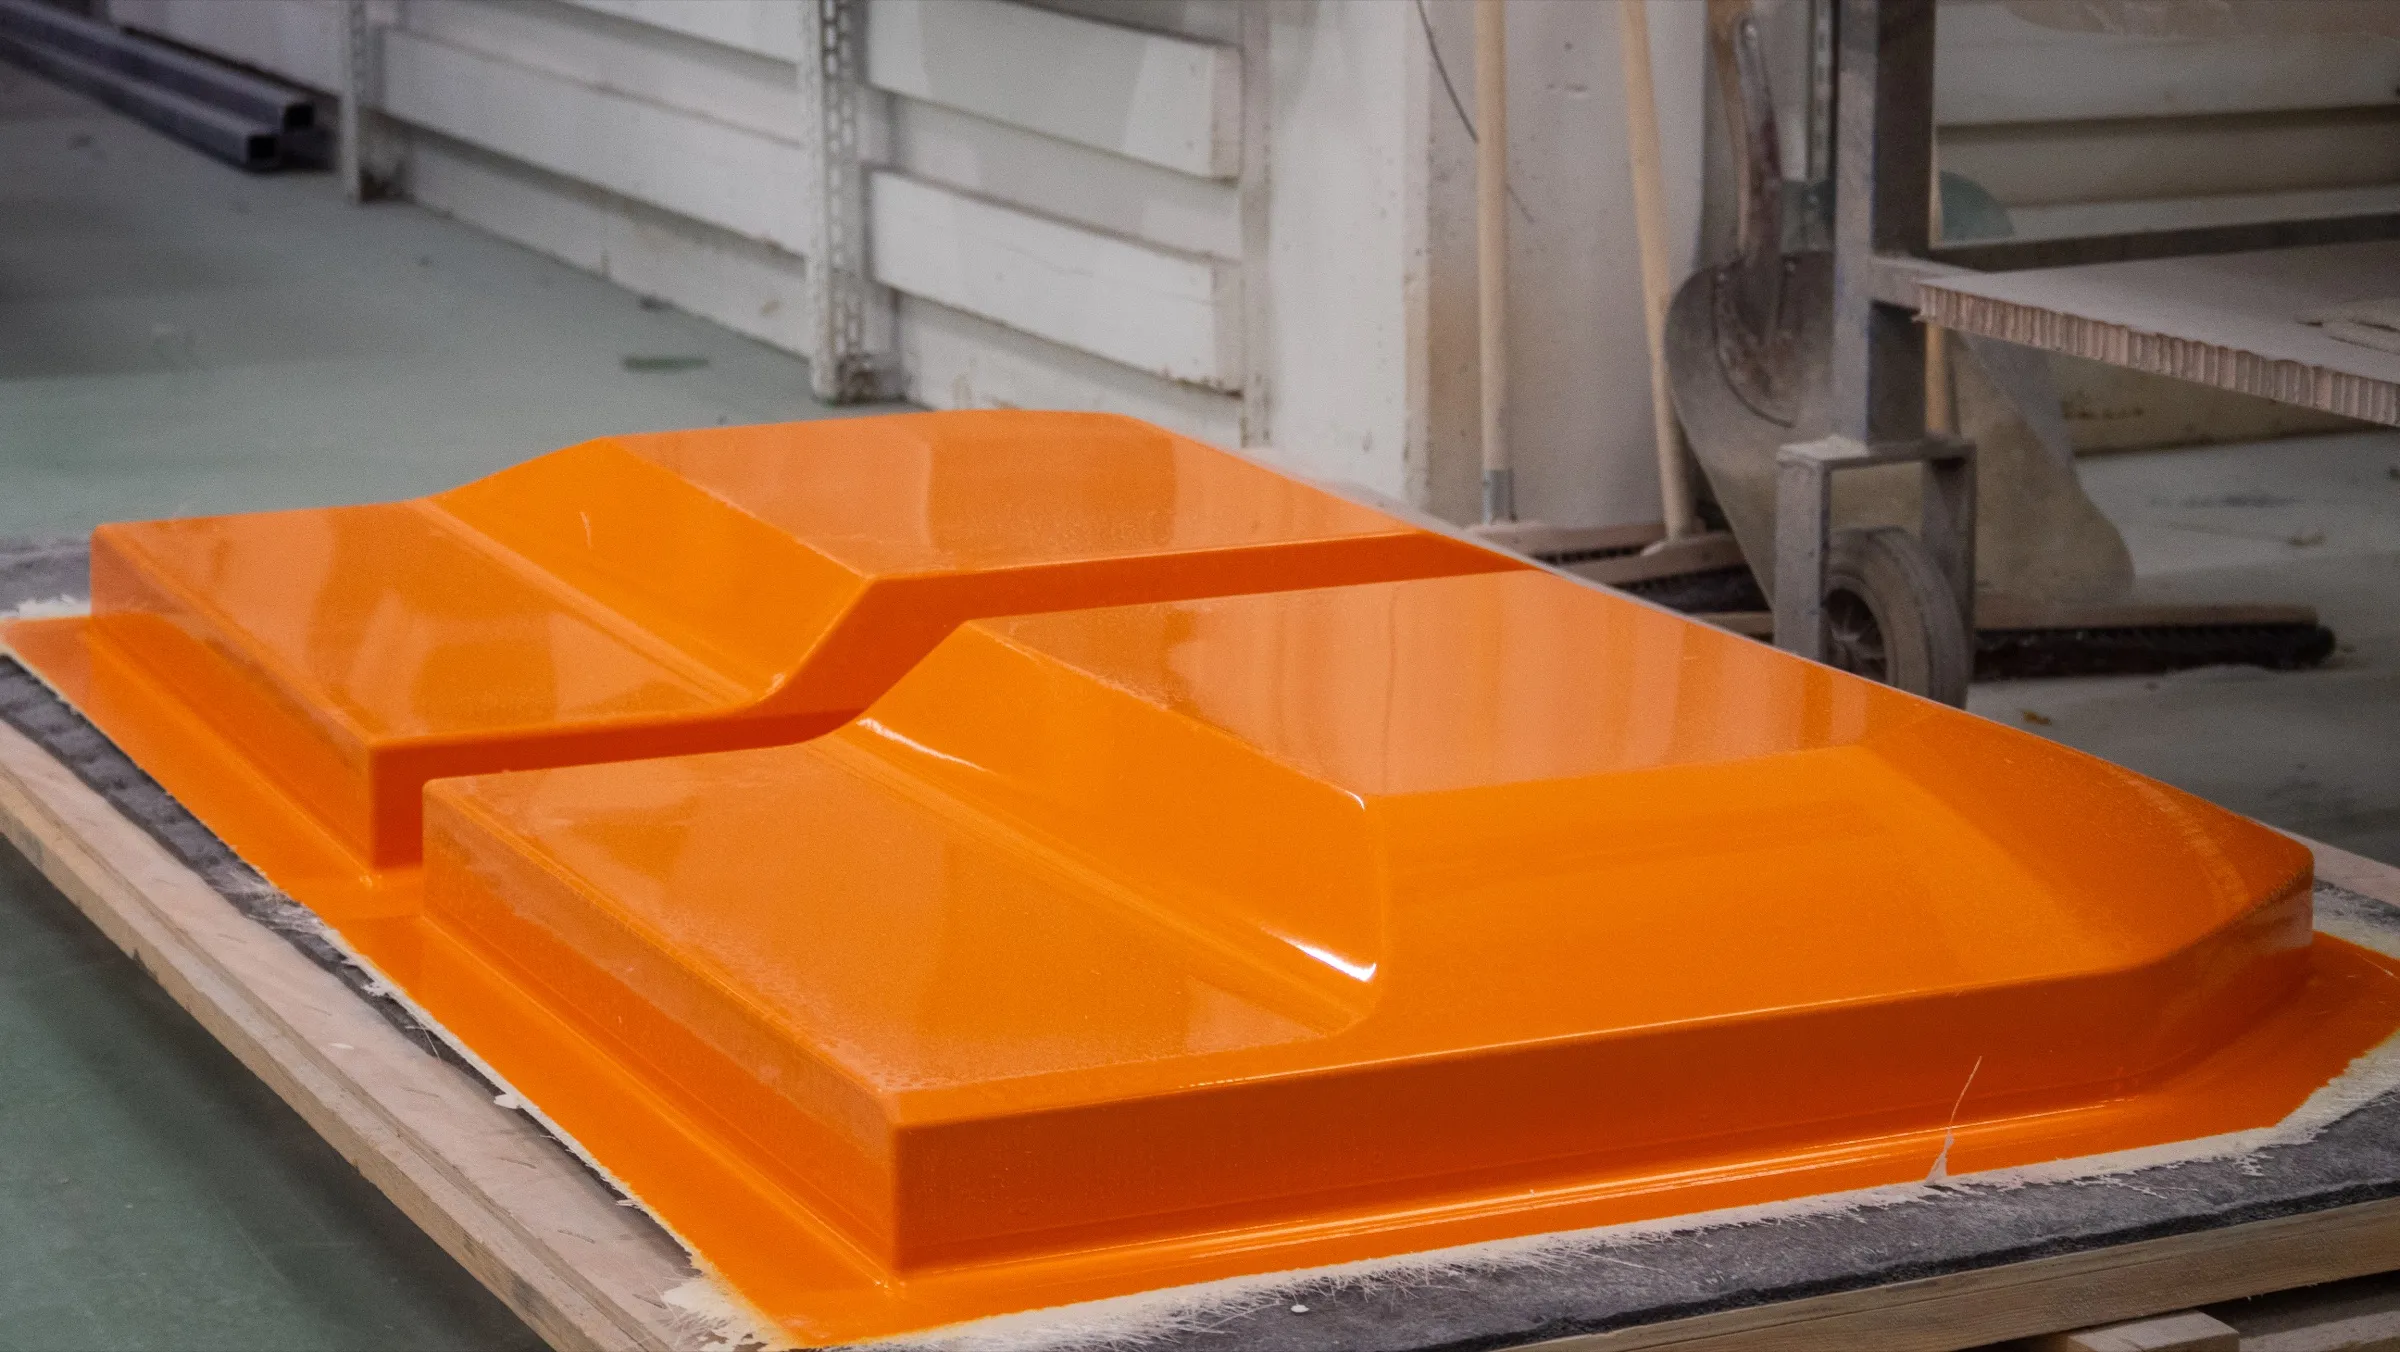
An orange plastic mould for composite manufacturing, set up in the workshop

System supplier and complete solutions

When Ljungby Komposit was established during 2009 we took over the necessary production equipment from Polytec Composites.

One example is our robotic water cutting equipment with a work area of 3500 x 2000 mm. It is specially adapted for parts with a large surface area, such as larger injected body parts (VARI, RTM) or volume products in SMC.

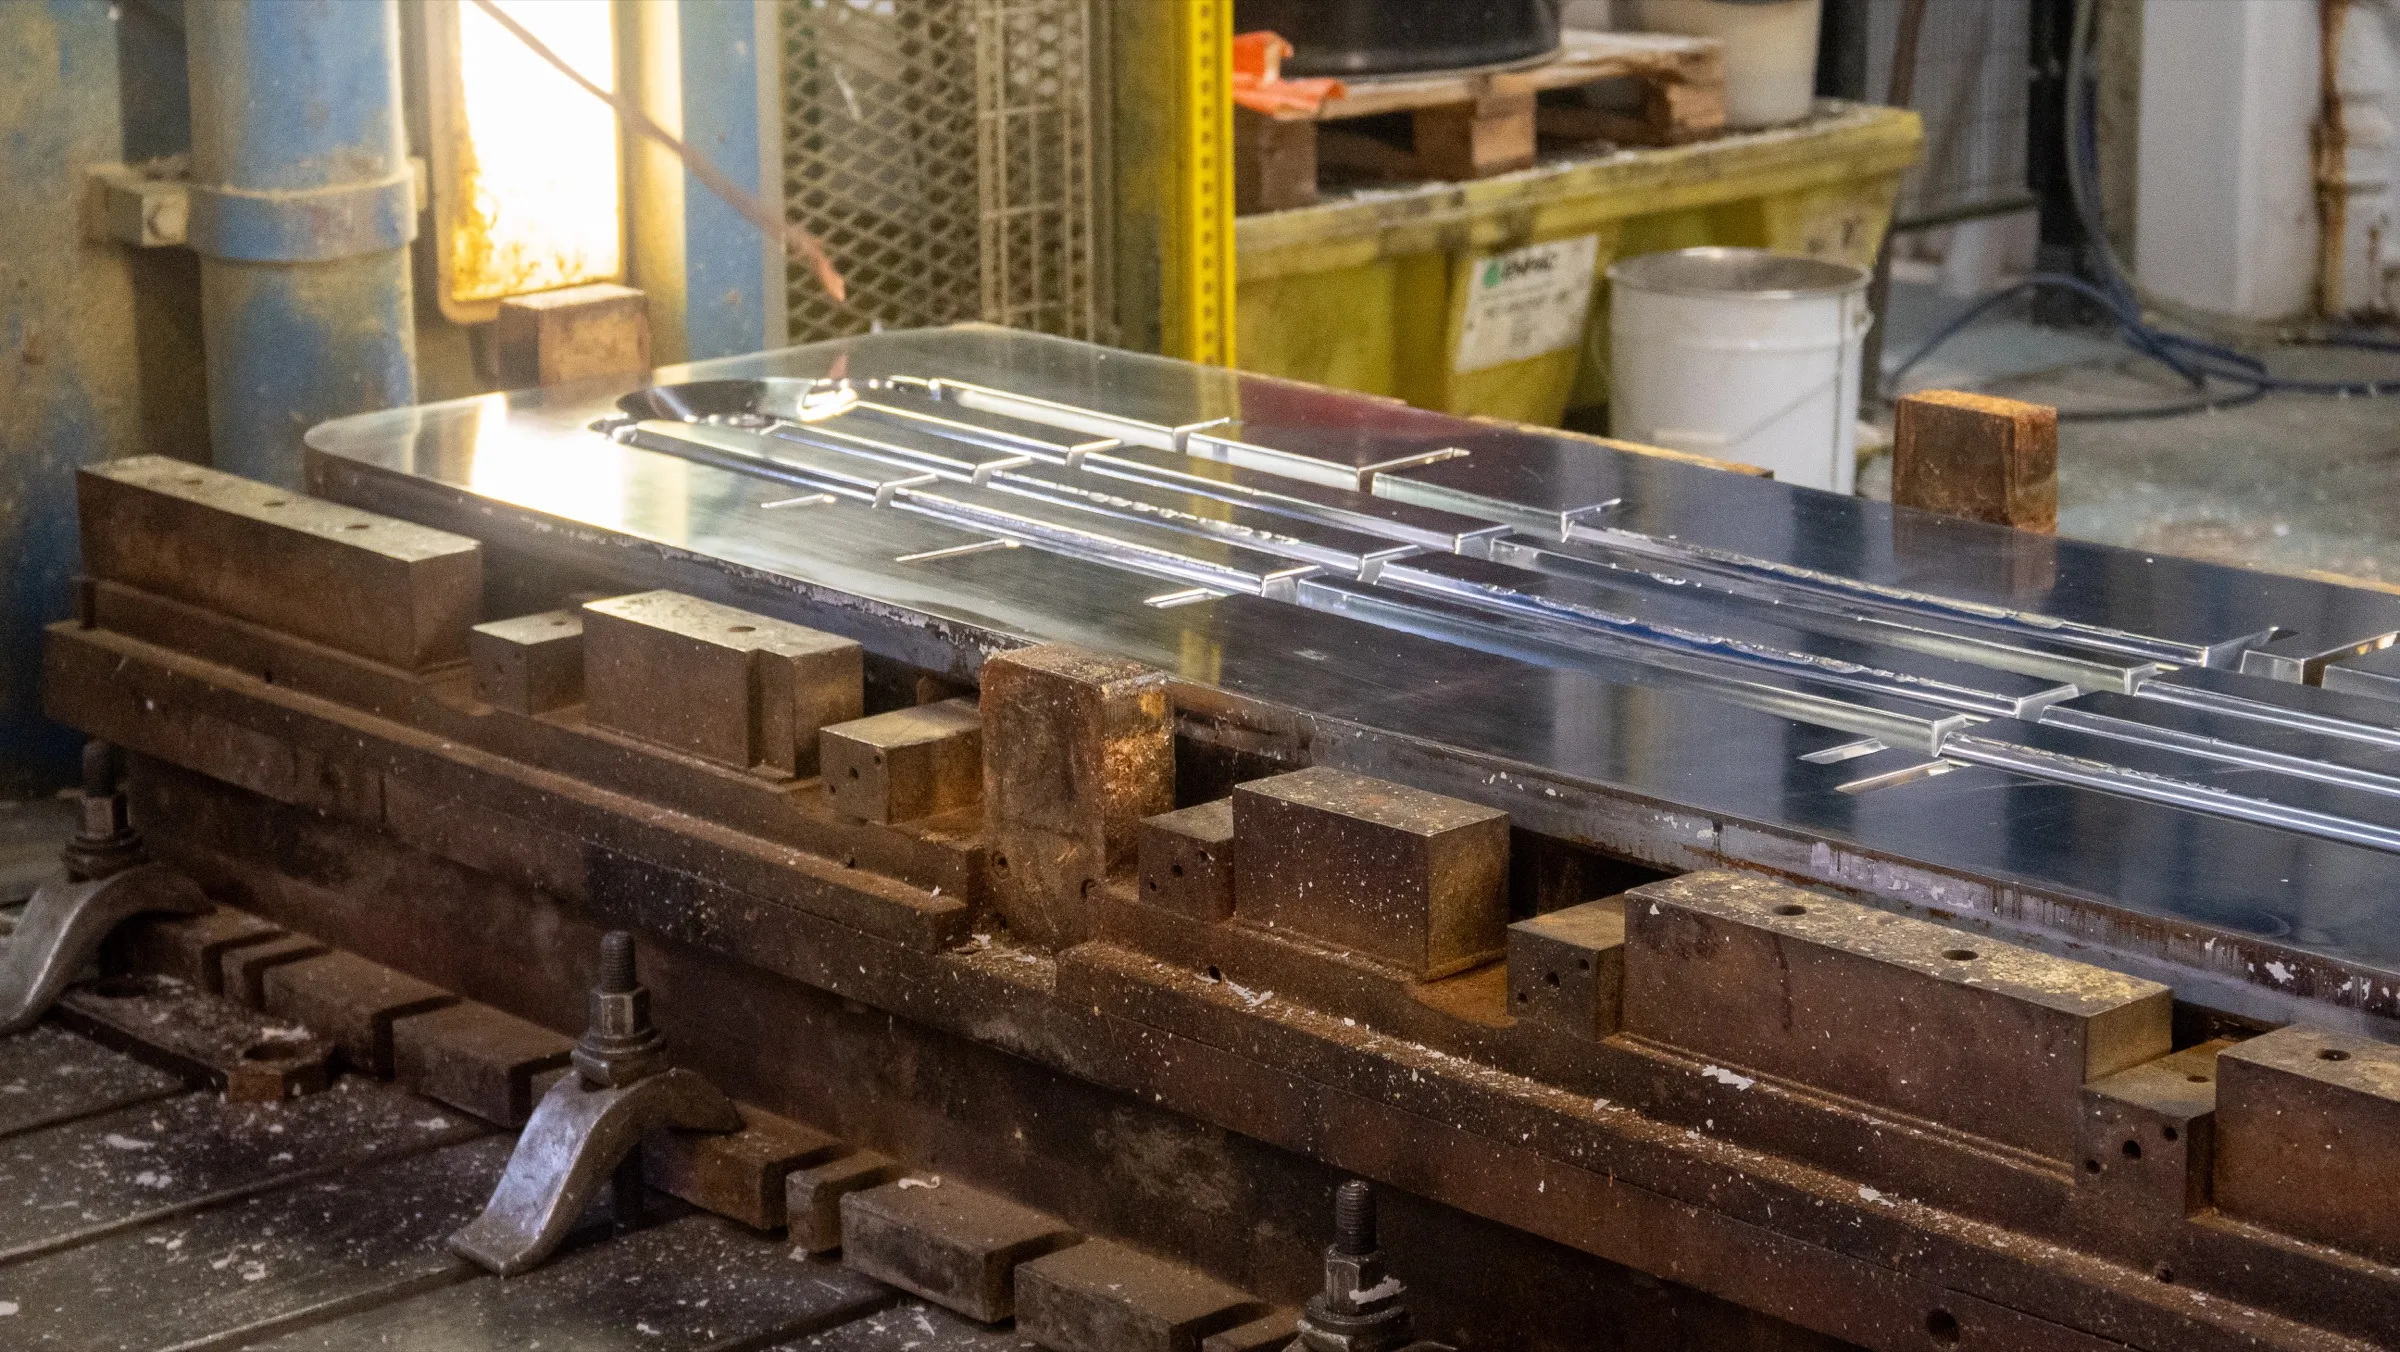
Another example is a hydraulic press with a press force of 1400 tonnes with a table size of 2500 x 2150 mm and an opening of 1900 mm. Everything to achieve cost effective production.

Our long industrial experience has provided us with a broad contact network, which has been further extended during recent years in order to strengthen our role as system supplier of complete solutions.
Efficient processes with great flexibility

There are many different types of fibre, many different plastics, different curing methods, different forming technologies, different ways of producing tools, etc.

In every situation it is important to evaluate, calculate and choose the combination of material and method depending on the objective. And there are often many unexpected approaches for solving or circumventing specific problems.

This is one of Ljungby Komposit's absolute strengths.

Processes

Manufacturing processes

There are many different types of fibre, many different plastics, different curing methods, different forming technologies, different ways of producing tools. In every situation it is important to evaluate, calculate and choose the combination of material and method depending on the objective.

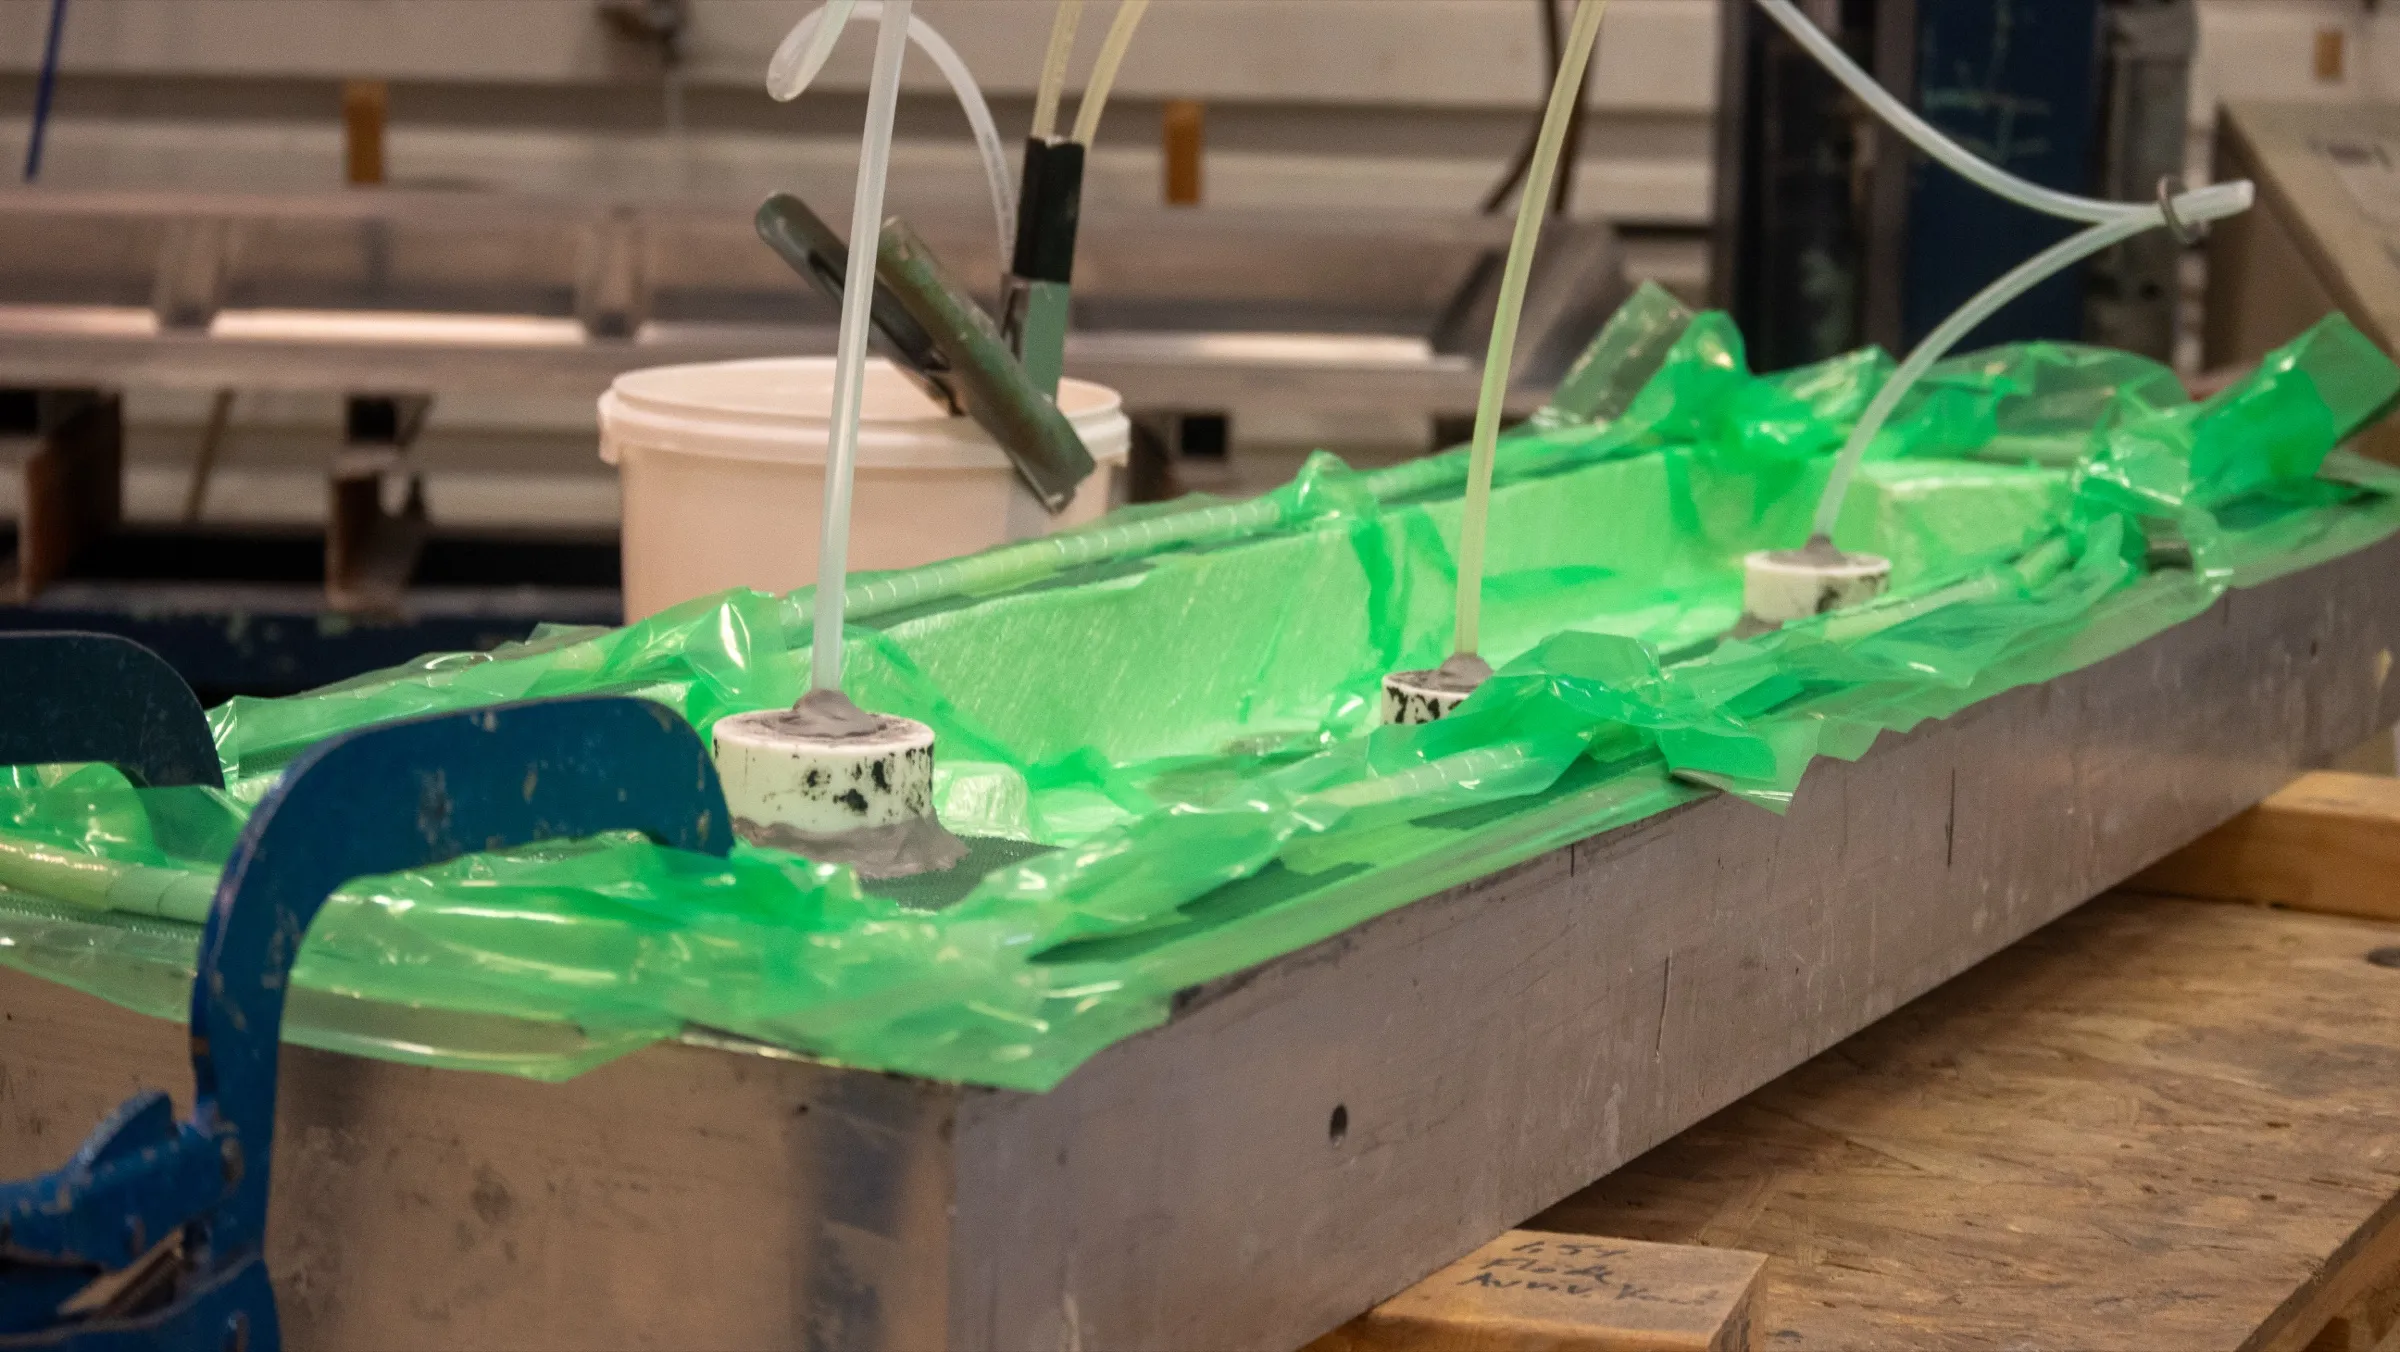
  • VARI Vacuum assisted resin injection Dry fibre is laid up in a closed tool and the resin is injected while the air is evacuated.

    The method is also called RTM Light. Dry fibre is laid up in a tool which is then closed, and mould halves produced in composite material are used here.

    The resin is injected into the fibre filled cavity using a pump that simultaneously mixes the two components of the thermosetting plastic. The air is evacuated with a vacuum pump to give optimal distribution inside the shell.

    The advantage is that tooling cost is kept considerably lower than with solid mould halves in metal. Gelcoat is usually sprayed onto the tool surfaces before the fibre is laid up. With coloured gelcoat, painting can be replaced, and the gelcoat can be mixed in any colour.

    Suited for Prototypes and series where tooling cost needs to stay down

  • RTM Resin transfer molding The same principle as VARI, but with solid tool halves in metal.

    RTM is equivalent to VARI in terms of the process, but instead of composite moulds, solid tool halves in metal are used.

    This gives better control of material thickness and dimensional accuracy. The tool can also be tempered, which reduces cycle time.

    Suited for Series with demands on dimensional accuracy and shorter cycle time

  • SMC Sheet mold compound Pre-impregnated glass fibre is pressed between heated steel tools under high pressure.

    Prepreg, meaning pre-impregnated glass fibre usually with polyester, is delivered ready on rolls. The material is cut according to a specified pattern and pressed between heated steel tools under high pressure.

    SMC pressing is a very stable process where every cycle is easy to monitor and log. The surface is easy to paint and dimensional stability is good. Other fibres can be used, but then under the term hot pressing.

    Suited for Larger series with demands on surface finish and dimensional stability

  • Cold pressing Cold pressing The fibres are laid up in an open tool and impregnated manually before the tool is closed in a press.

    The fibres are laid up in an open tool and impregnated manually before the tool is closed in a press.

    The method suits prototypes and short series. Emission to the surroundings is not insignificant, unlike the methods that take place in closed tools.

    Suited for Prototypes and short series

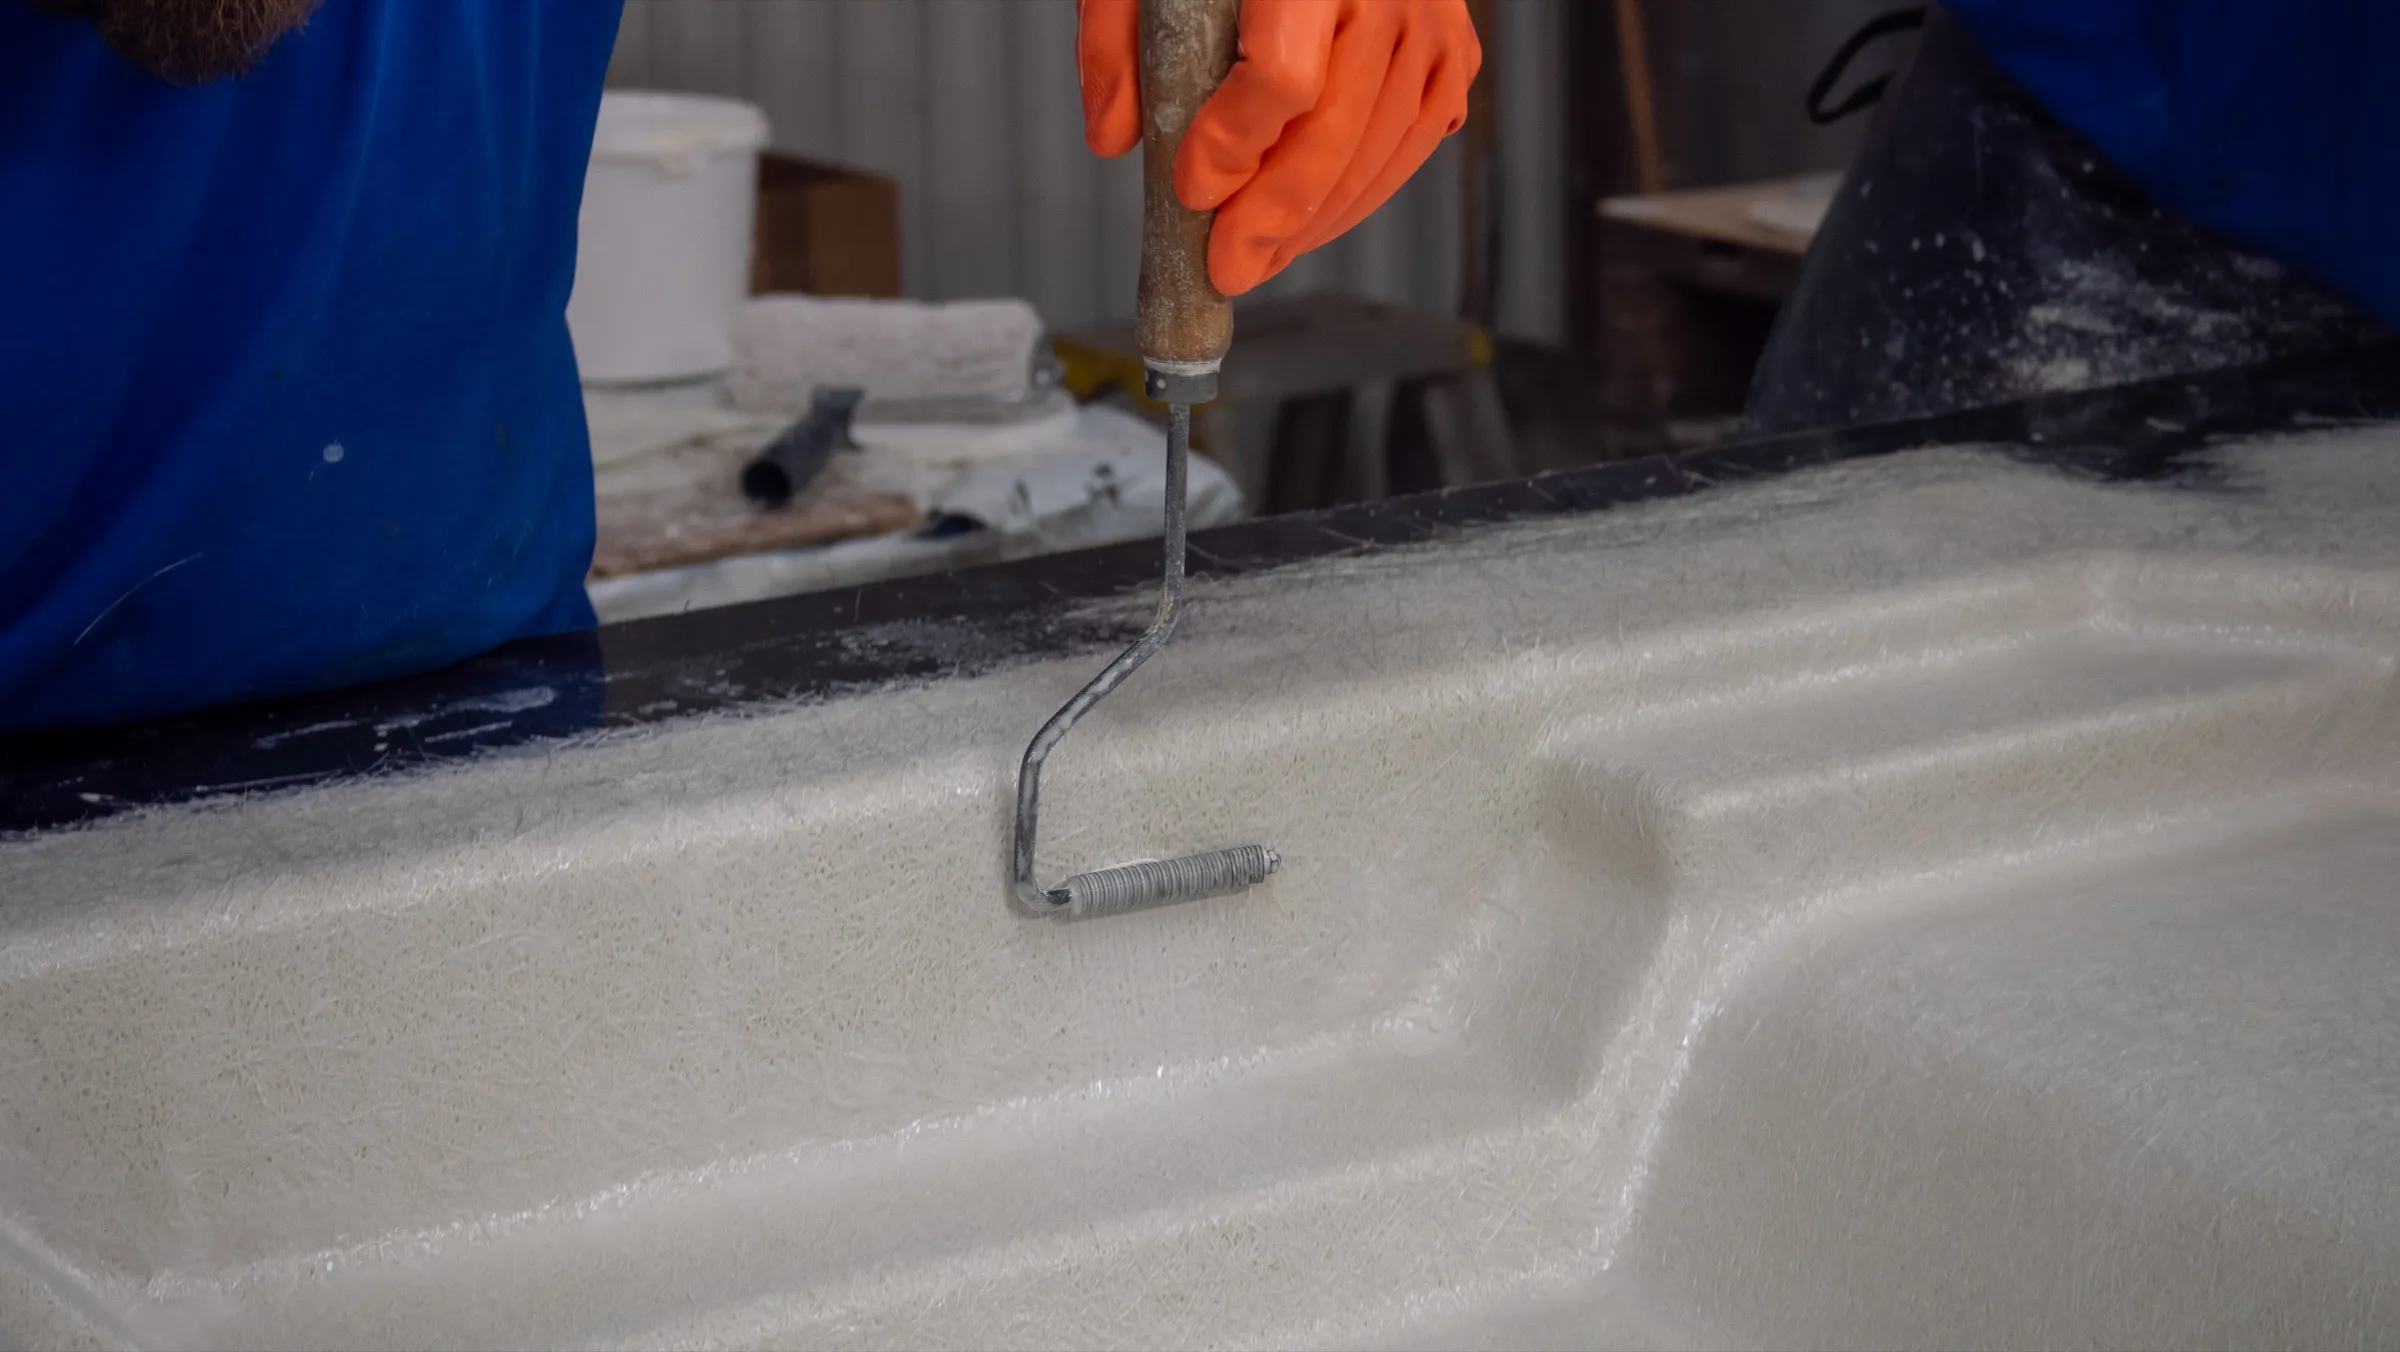
  • Hand lay-up Hand lay-up An open process with low tooling investment.

    Hand lay-up is suited above all to short series and prototypes.

    It is an open process with low tooling investment, which makes it useful when the volume is too small to justify a metal tool.

    Suited for One-off manufacturing, prototypes and very short series

System supplier and complete solutions

  • Robotic water cutting Work area 3500 × 2000 mm. Adapted for parts with a large surface area, such as injected body parts and volume products in SMC.
  • Hydraulic press 1400 tonnes of press force, a table size of 2500 × 2150 mm and an opening of 1900 mm.
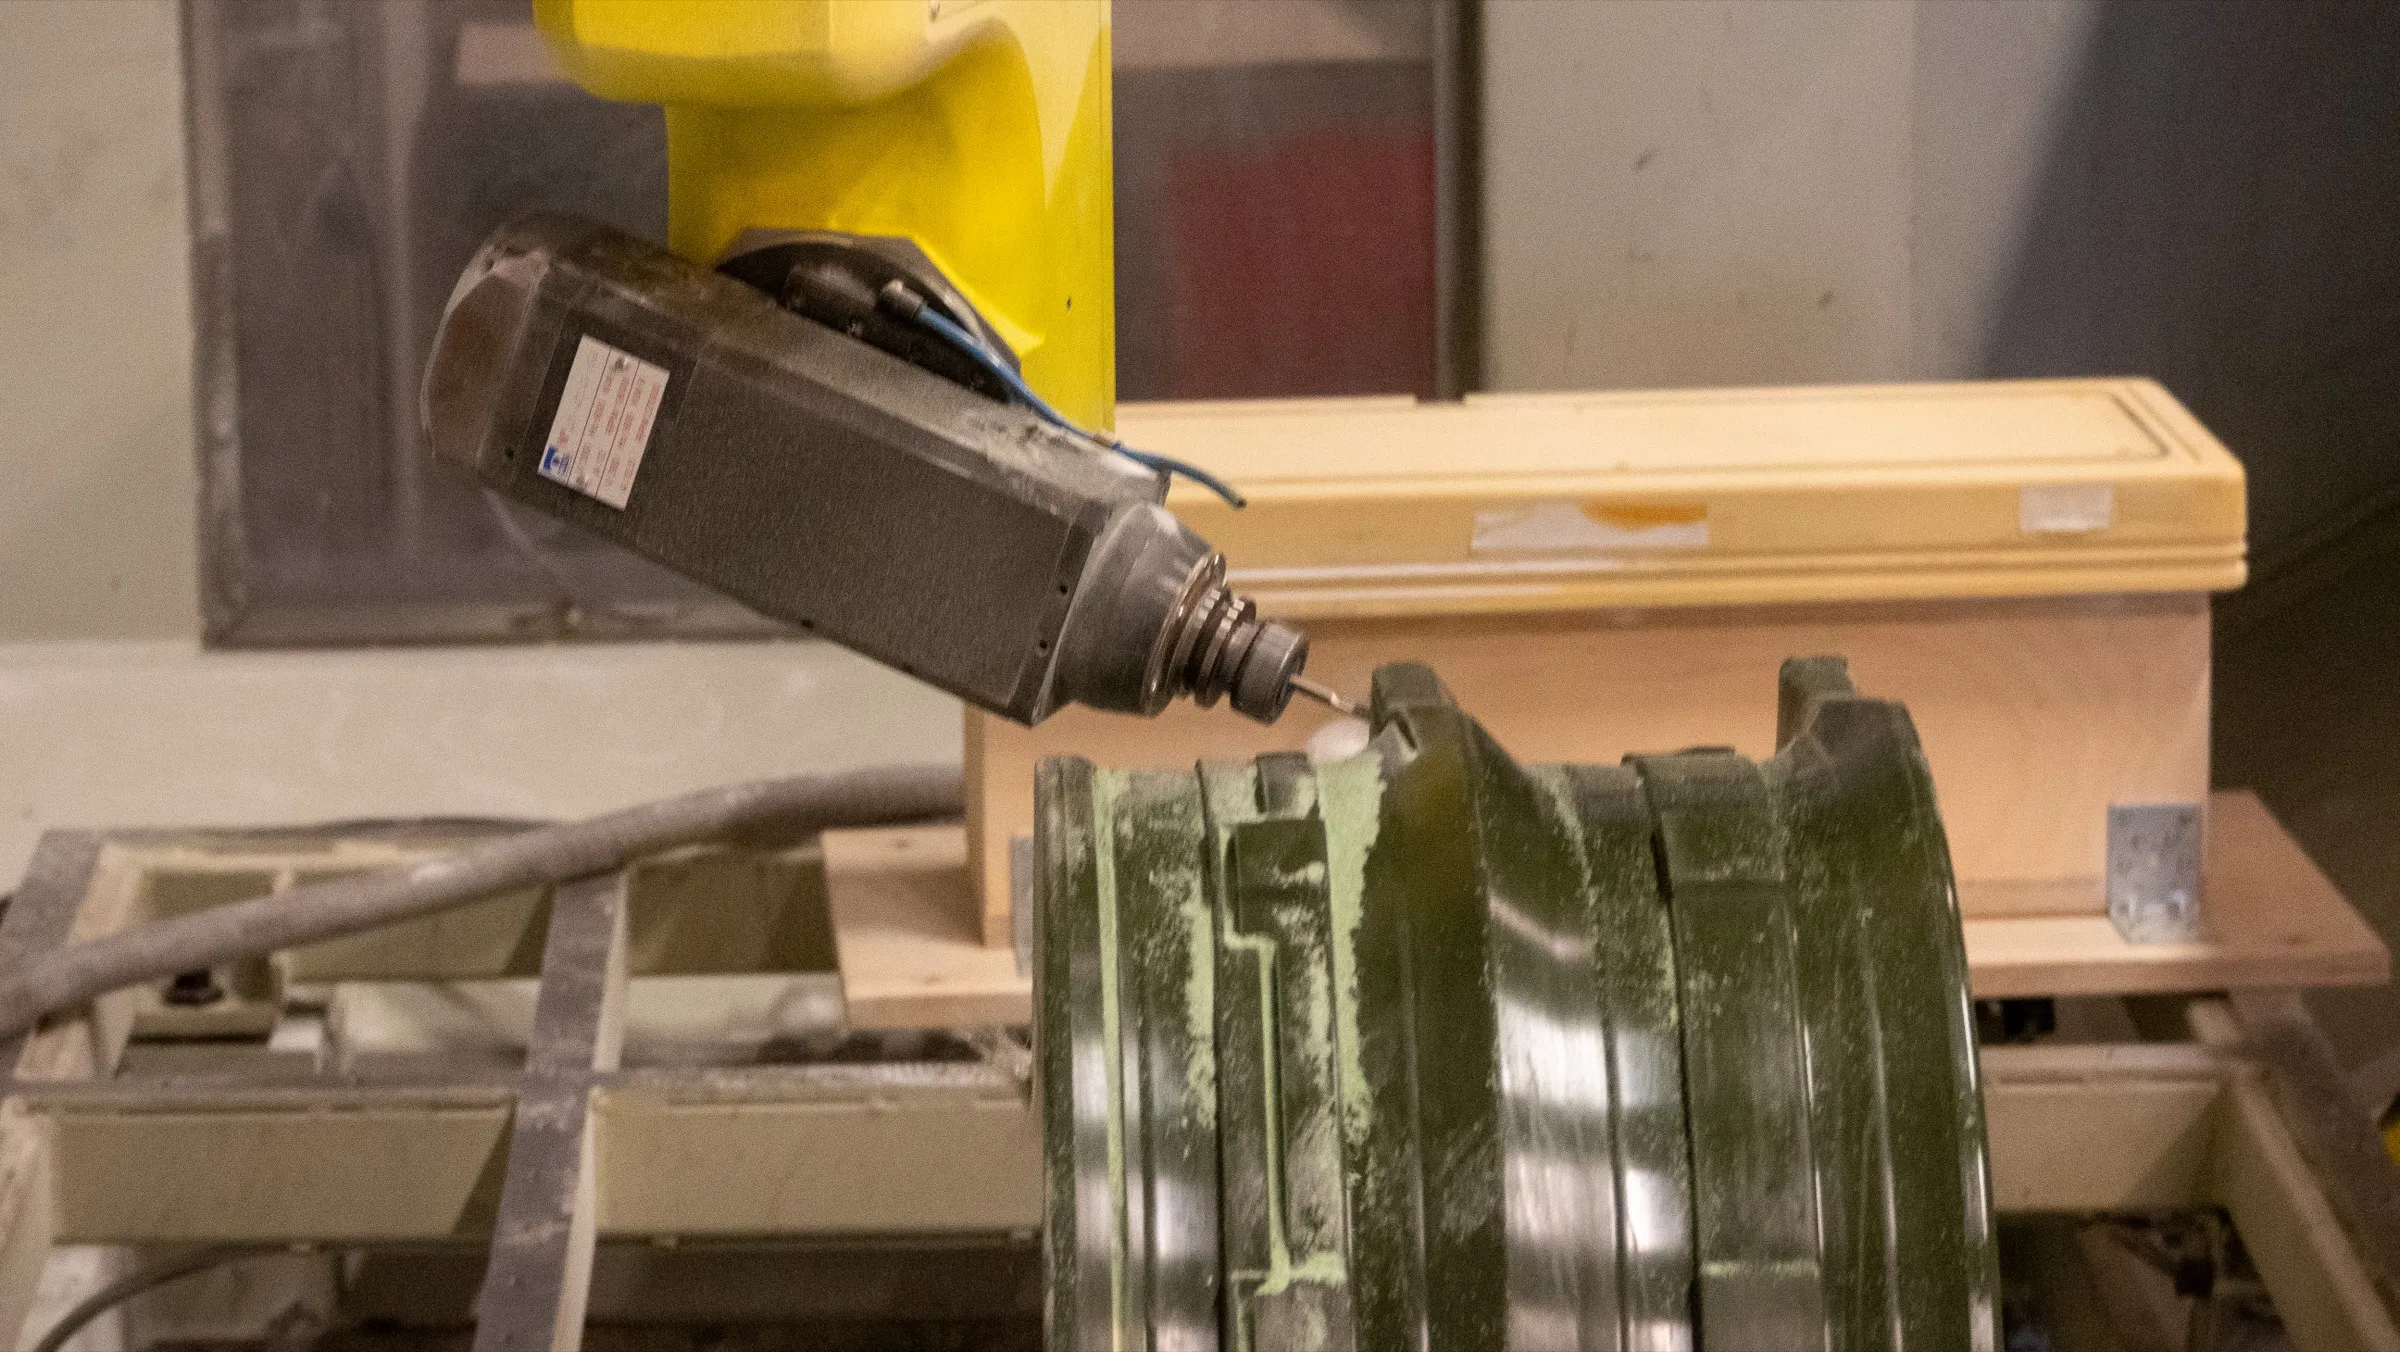
  • CNC router CNC-controlled 5-axis milling machine for large parts, 4800 × 2000 mm.

In the workshop

  • Mould covered with vacuum film and hoses for resin infusion
    Mould covered with vacuum film, with hoses for resin infusion.
  • Colleague laminating by hand with a roller against a mould
    Hand lay-up, working the roller against the mould.
  • Steel tool clamped in the hydraulic press
    Steel tool clamped in the hydraulic press.
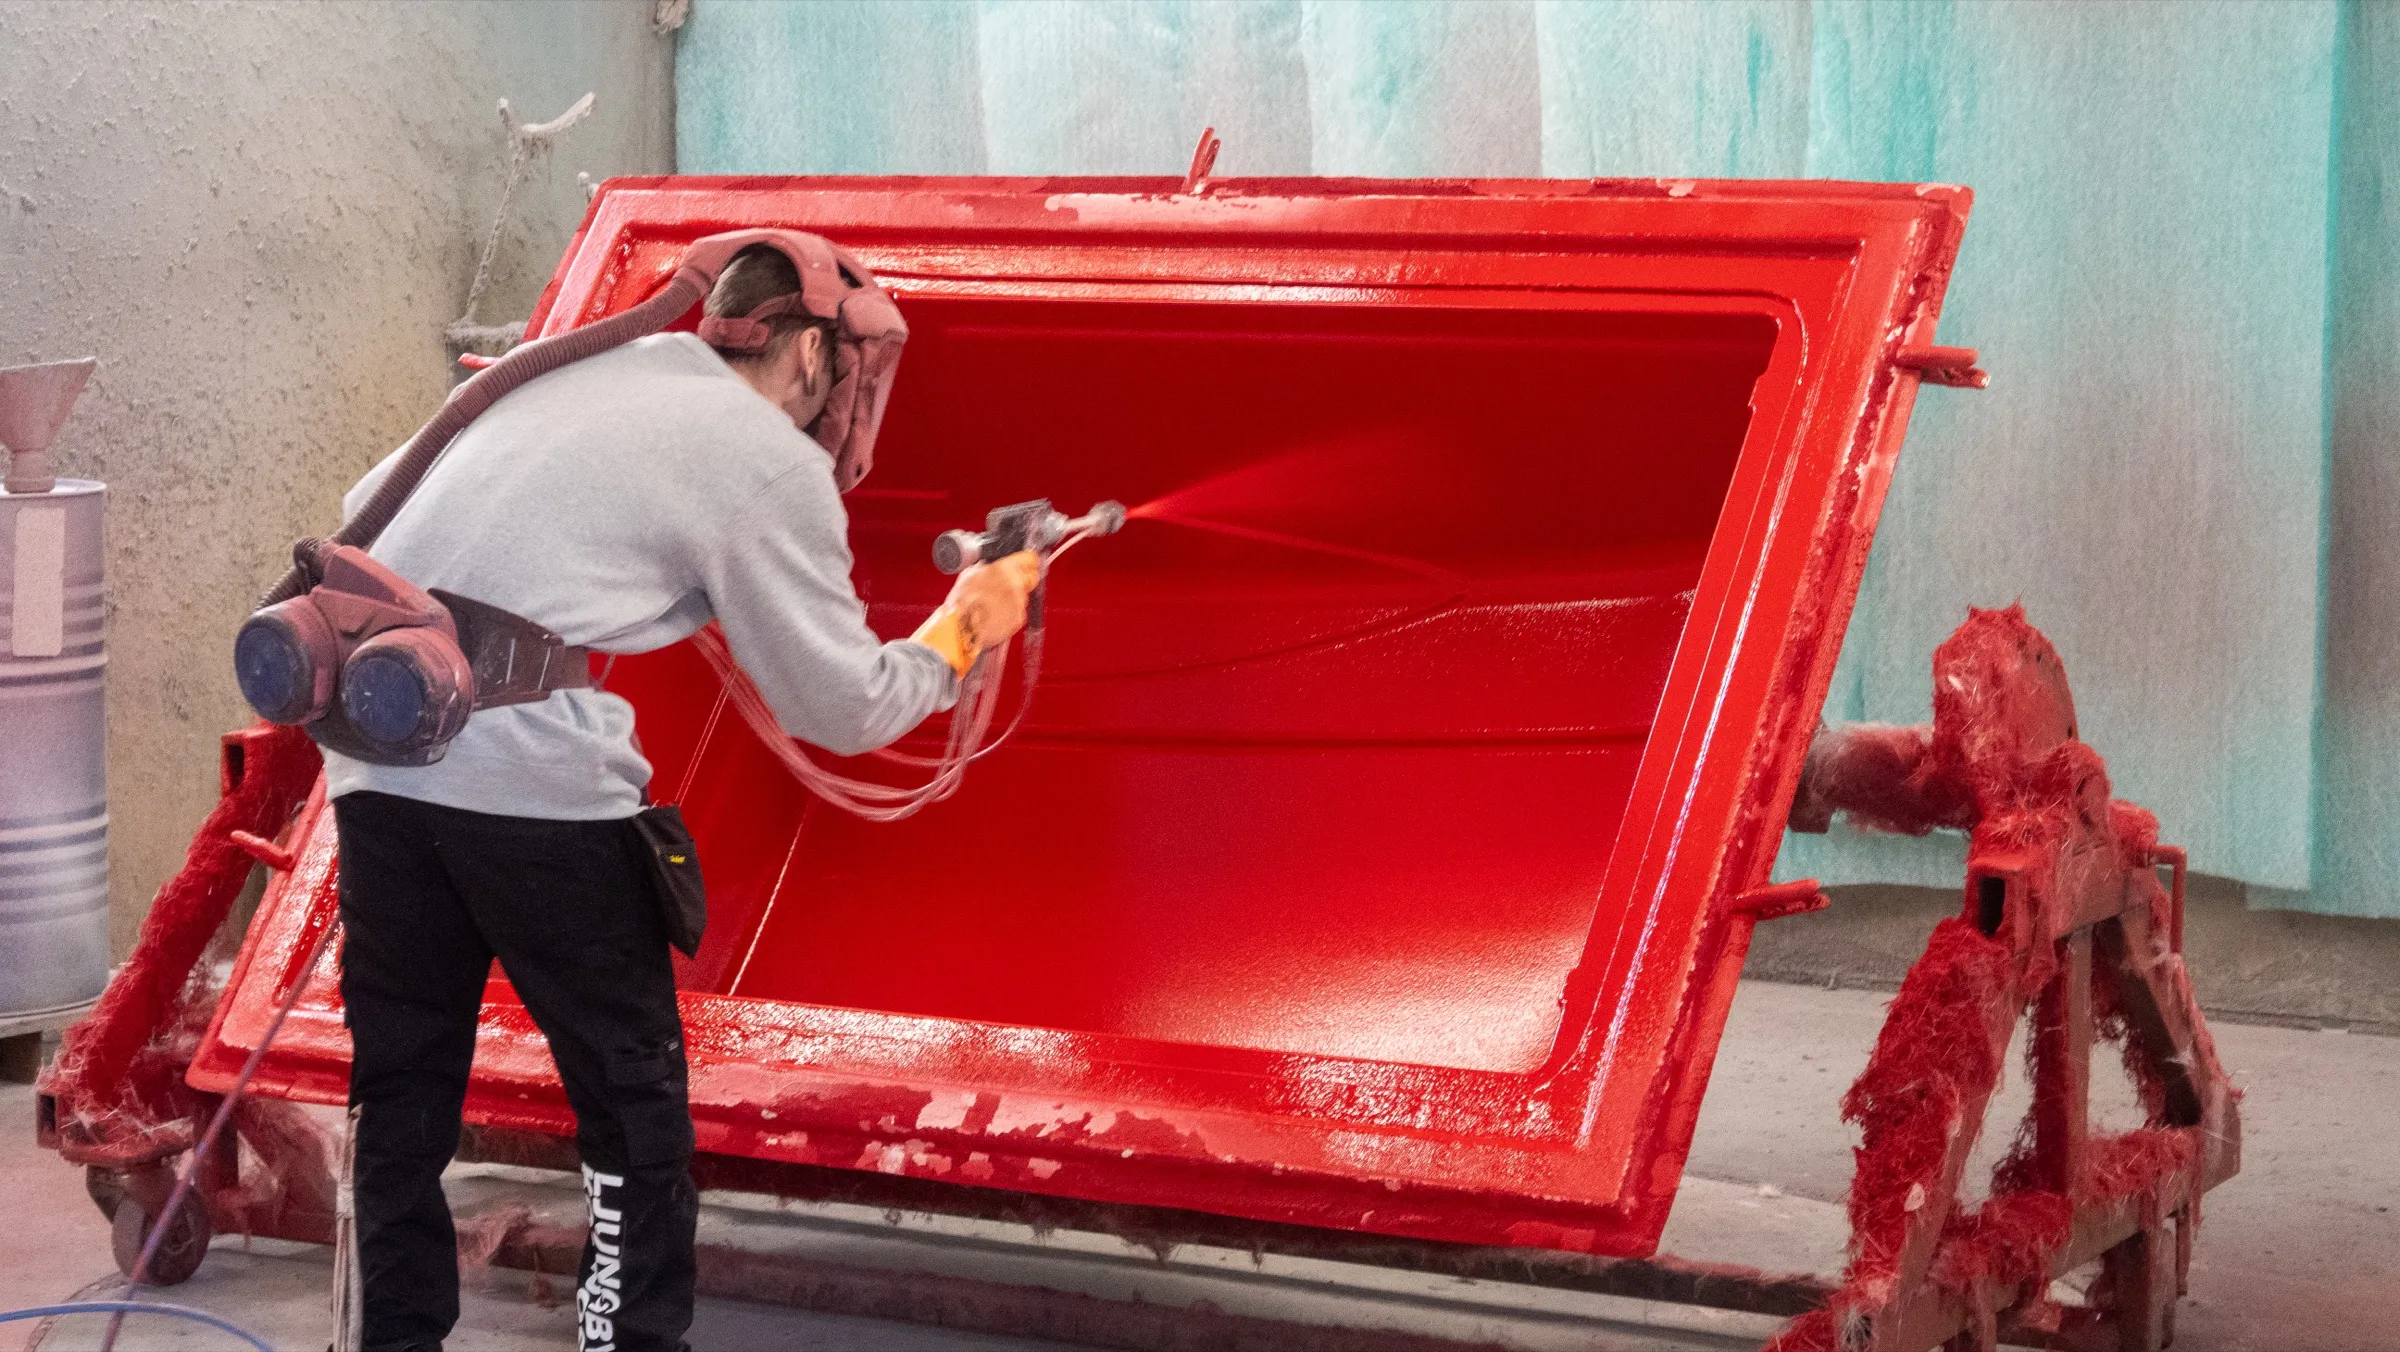
  • Colleague spraying surface coating inside a mould in the spray booth
    Surface coating sprayed into a mould in the spray booth.
  • Robotic milling of a mould in the workshop
    Robotic milling of a mould in our own tool making.
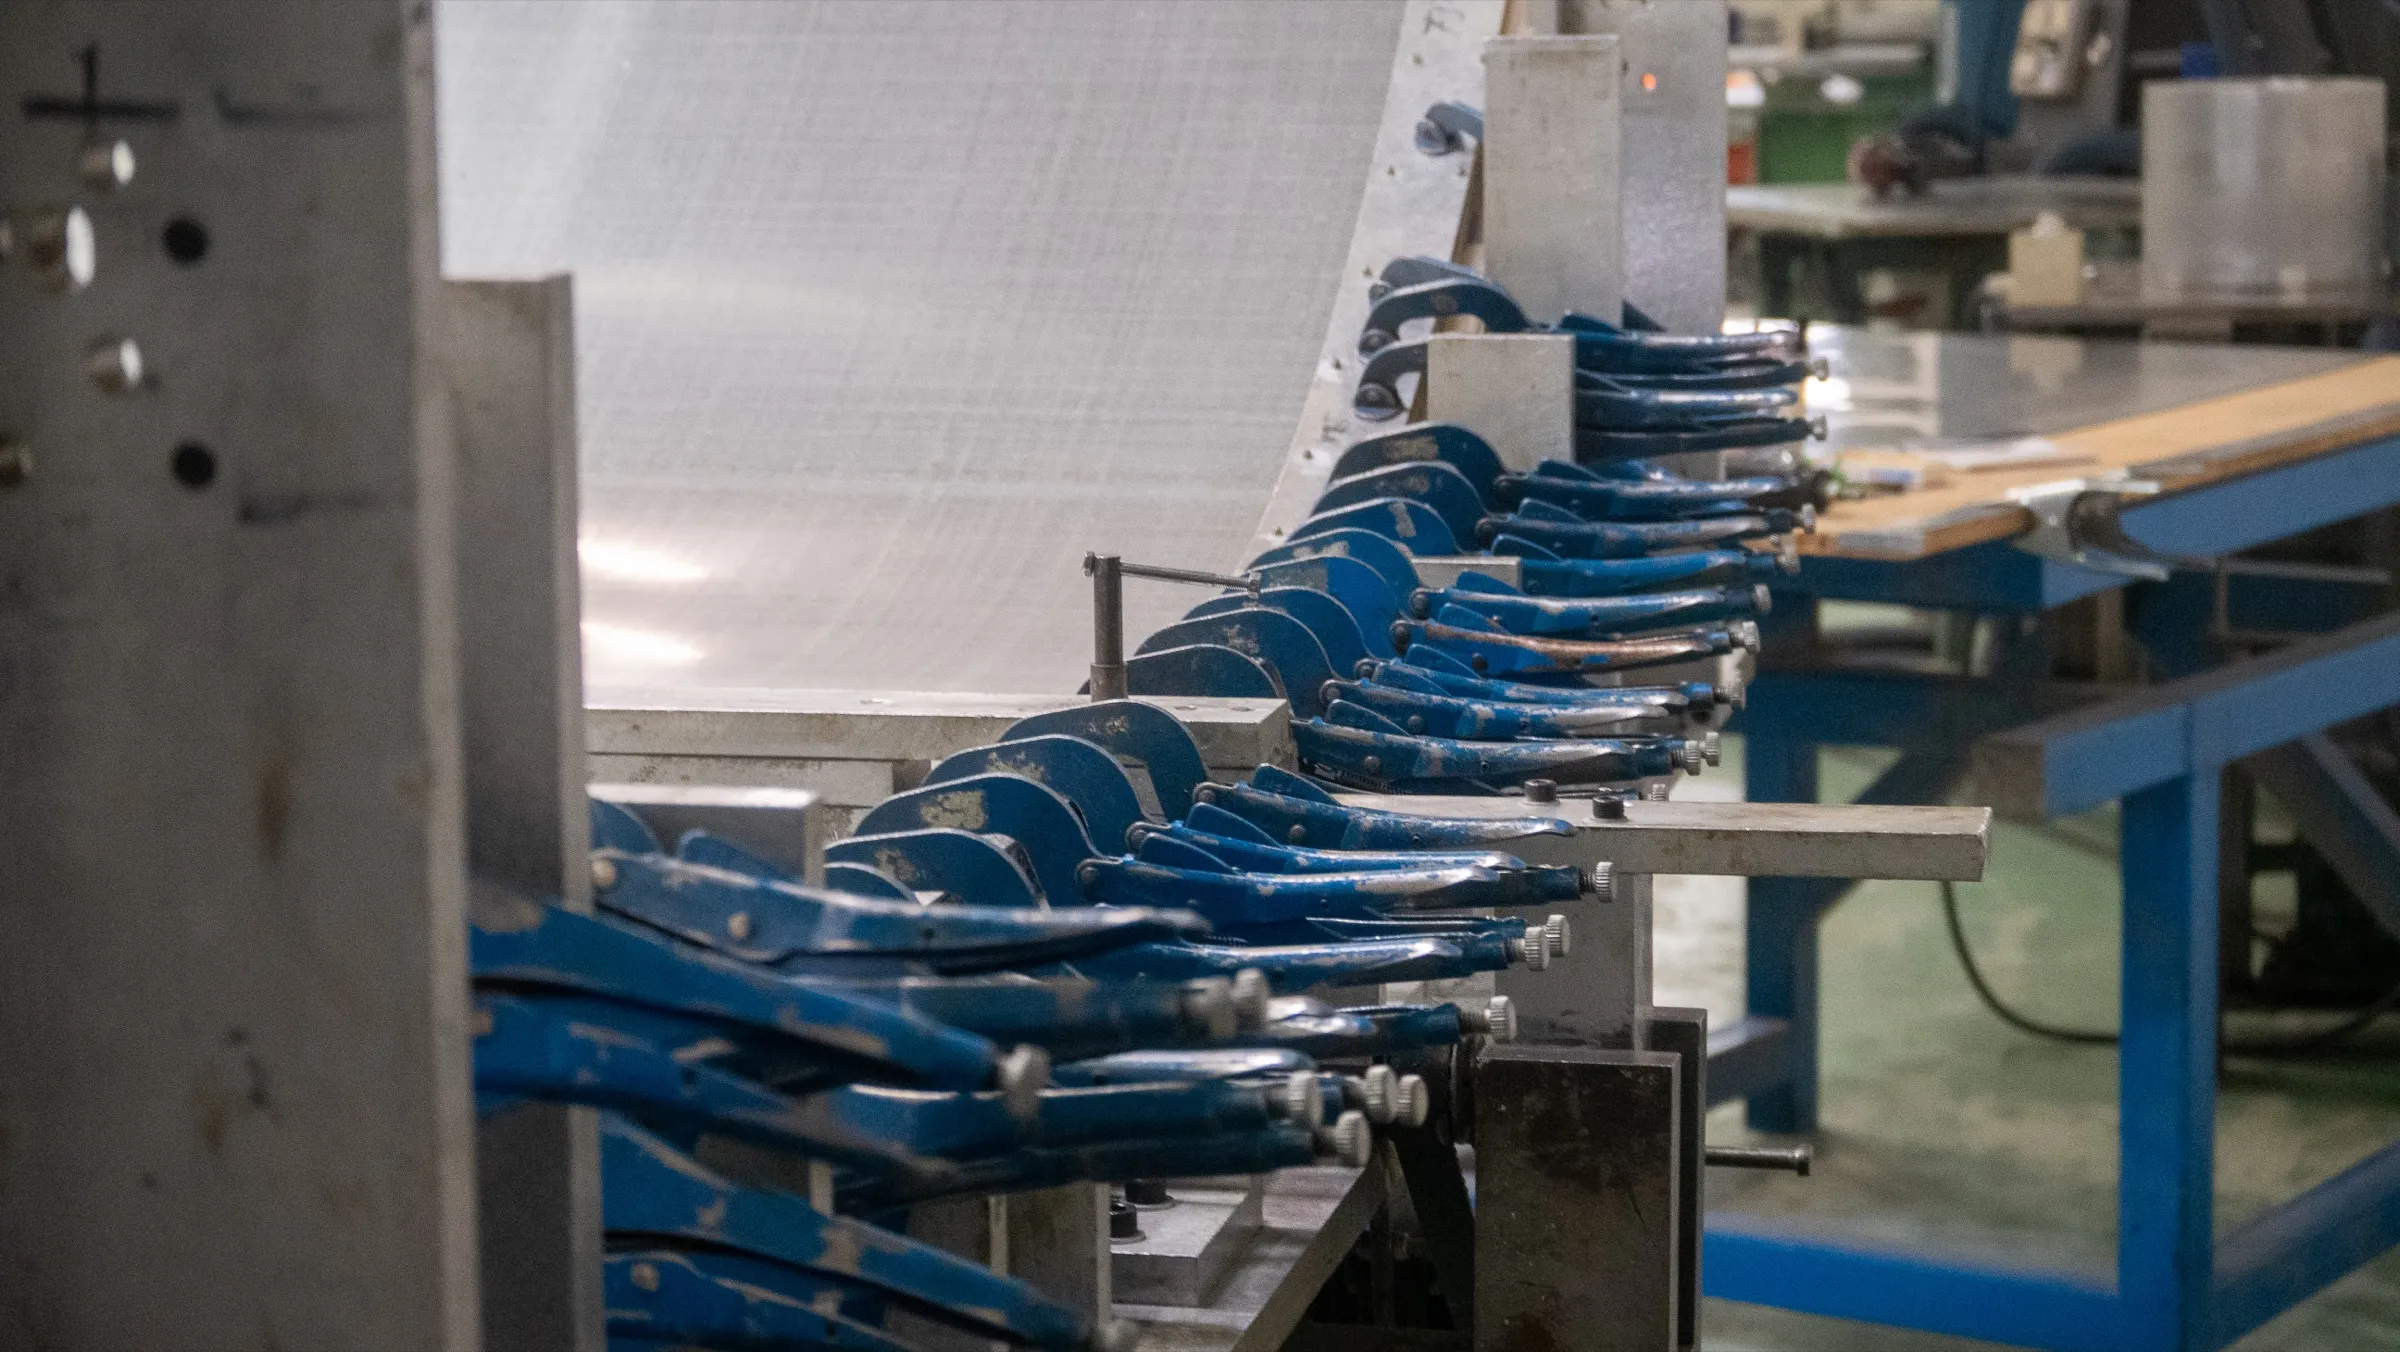
  • Row of clamps along the edge of a mould
    Clamps hold the mould closed along its full edge.
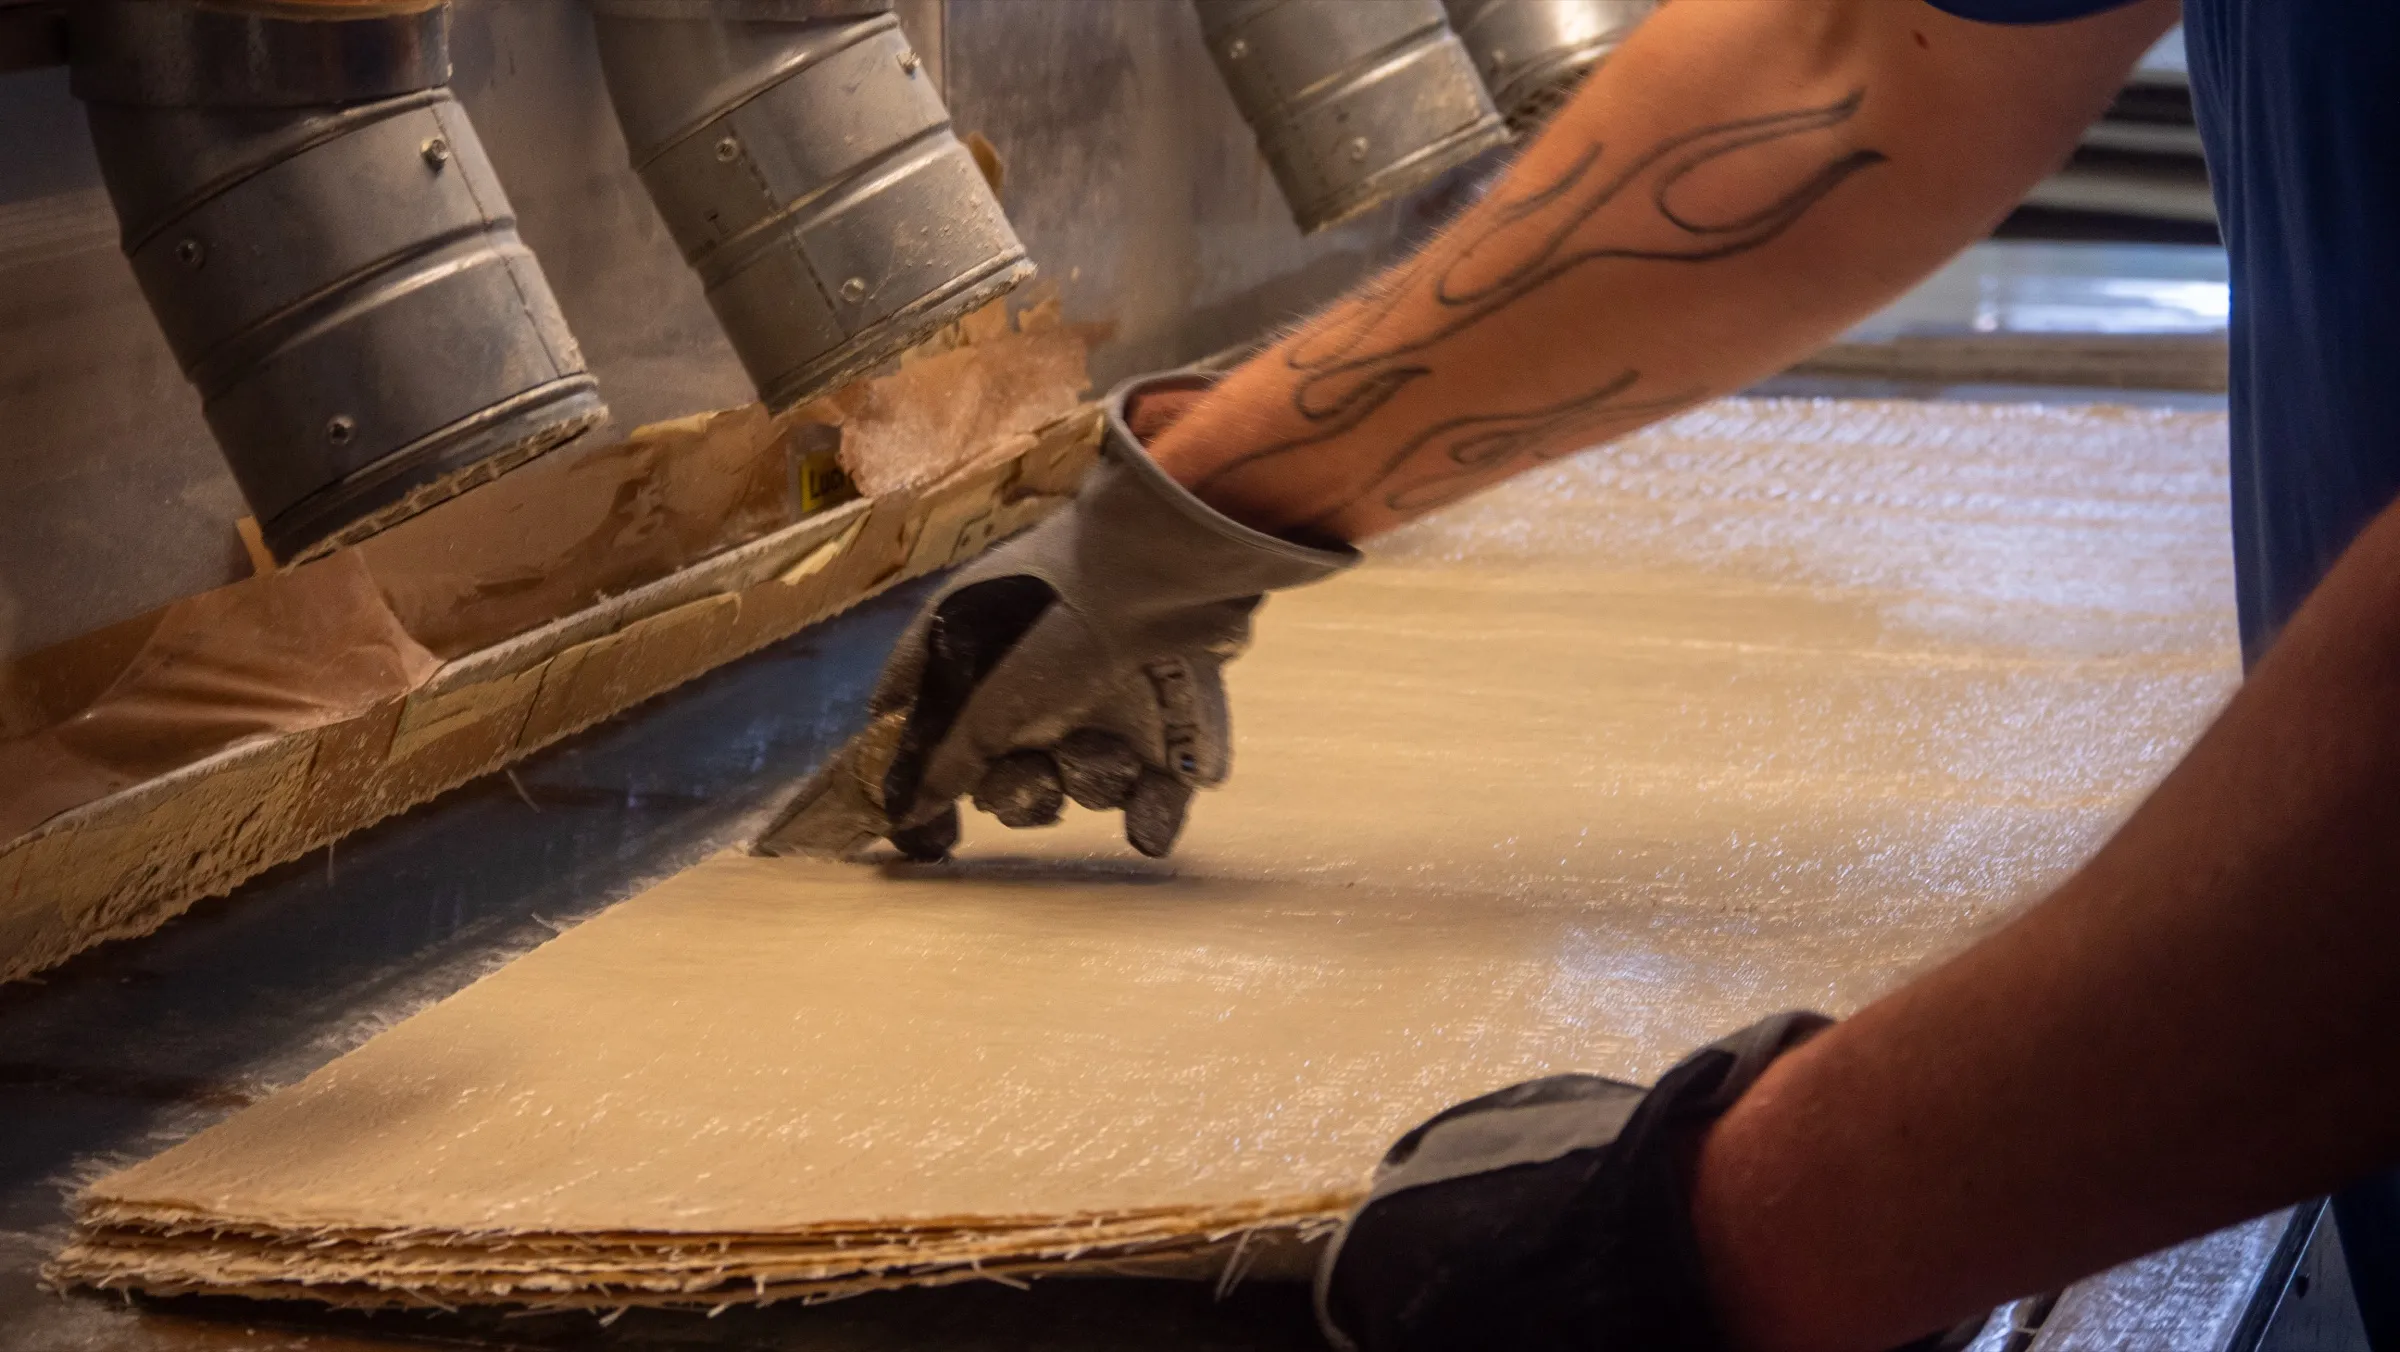
  • Colleague positioning a reinforcement mat by hand
    Reinforcement mat positioned by hand.
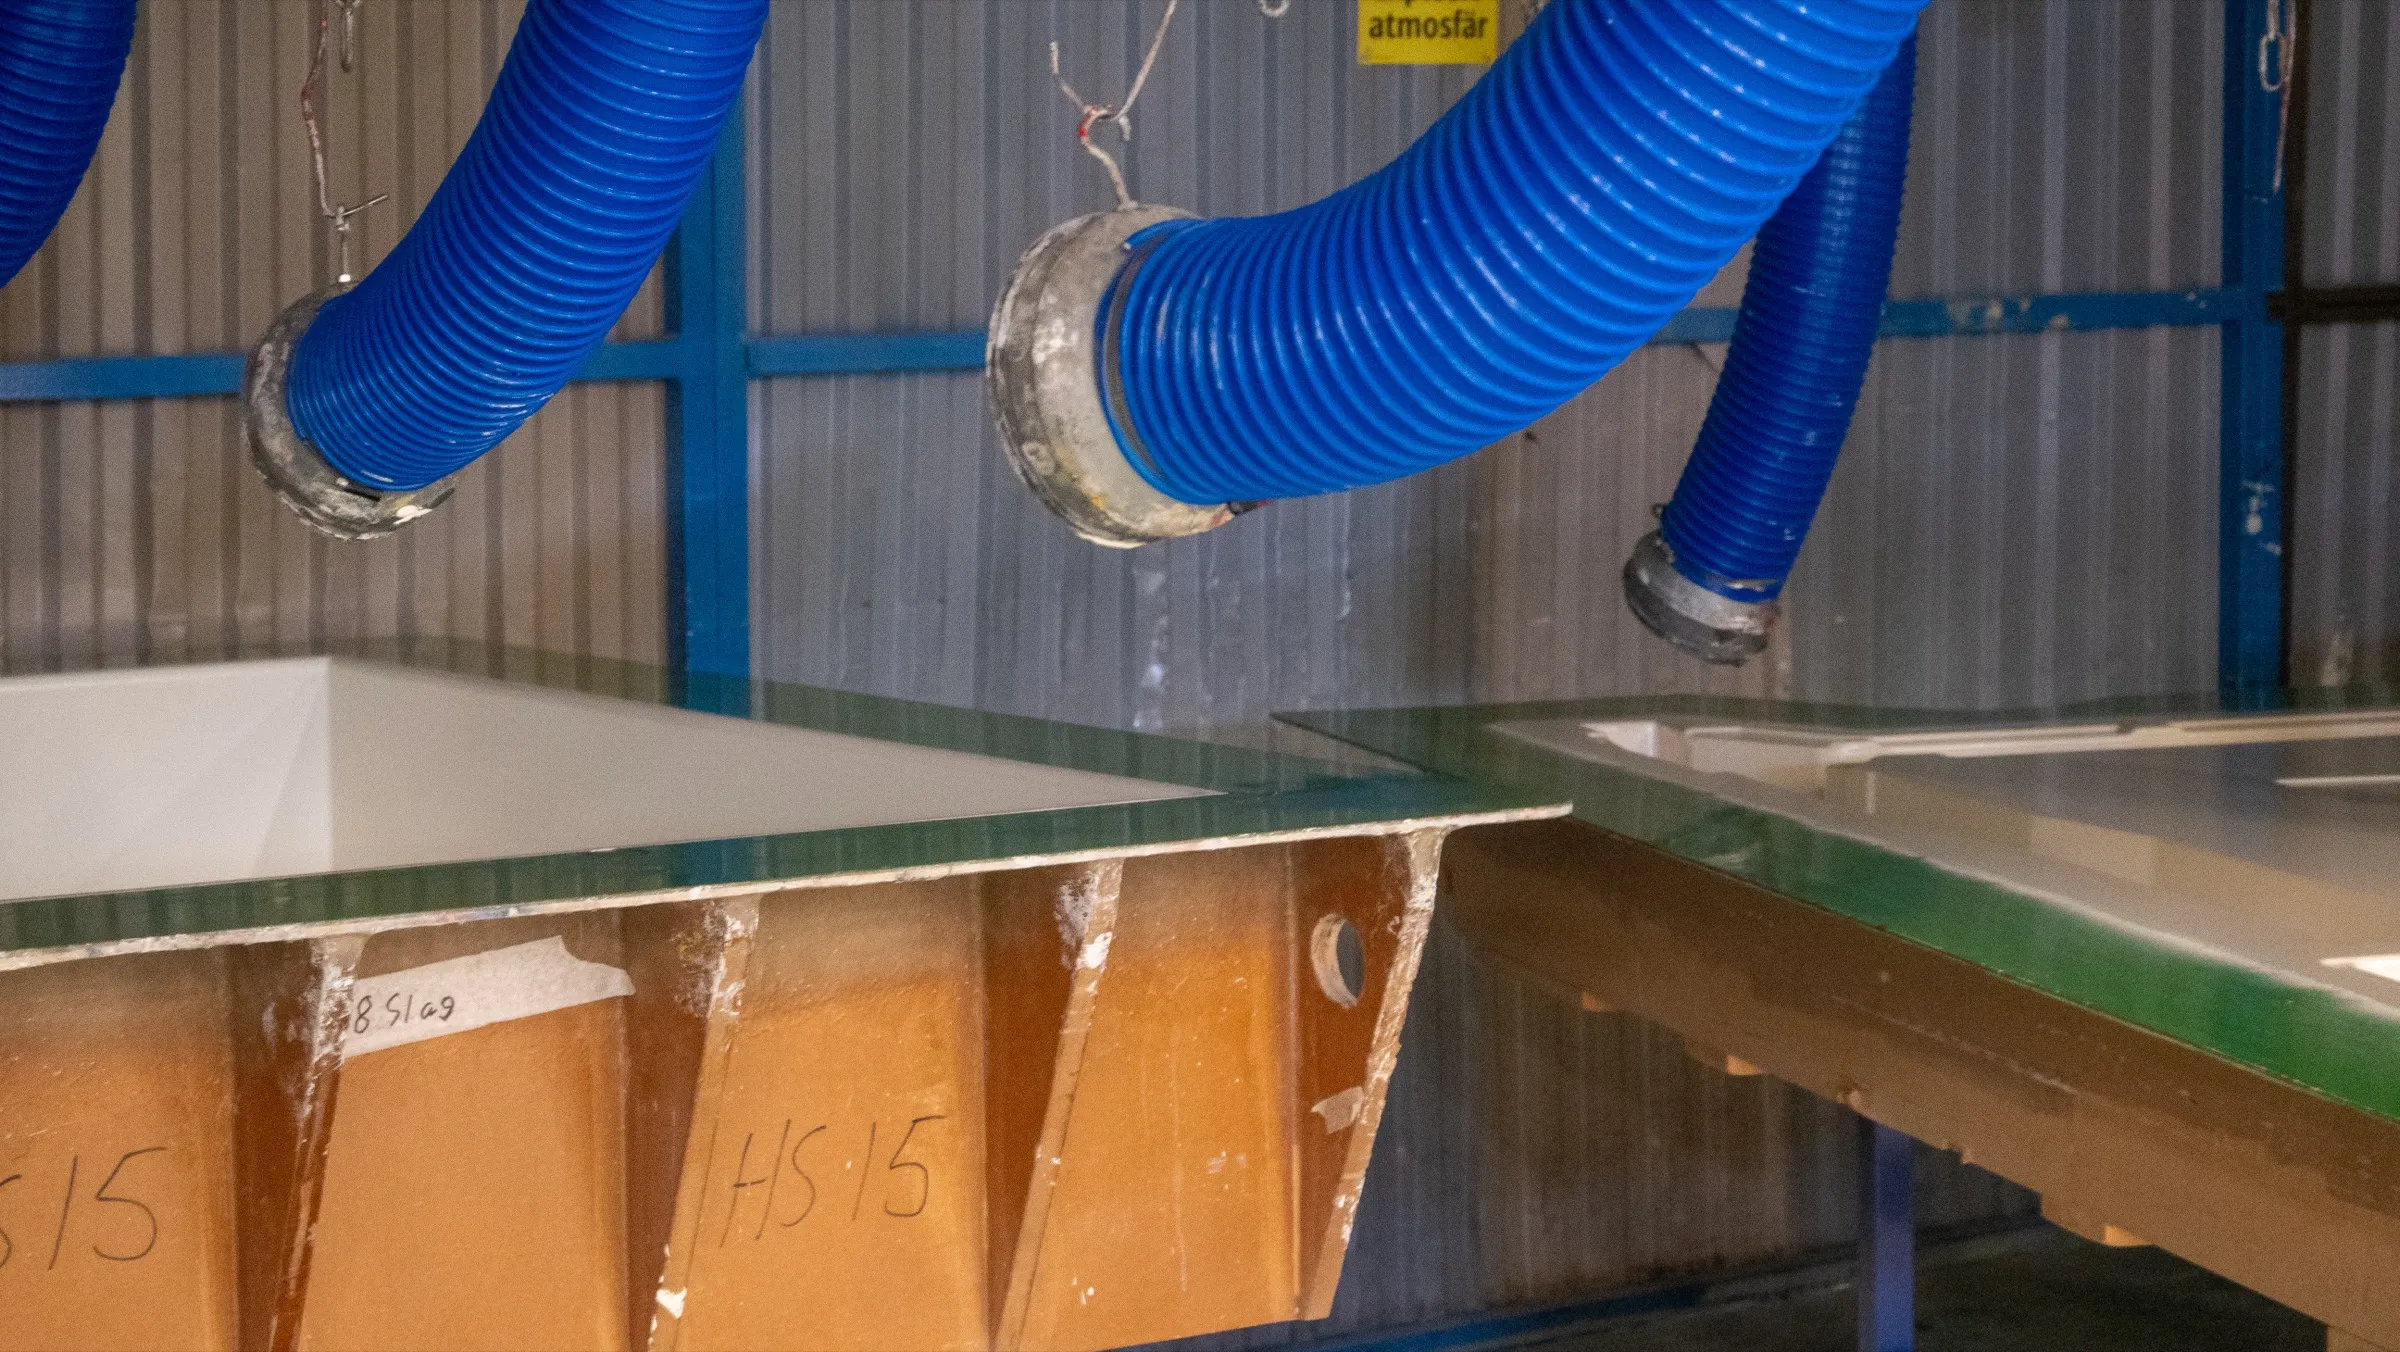
  • Extraction hoses above moulds in the lamination room
    Extraction above the moulds in the lamination room.

Think innovative solutions

Talk to us at an early stage in your product development work. Then will both of us feel much better, because in the end of the day this is always a matter of costs, investments and pay-off for both parties. Welcome!